


Concise Course in the Fundamentals of Stamping Theory
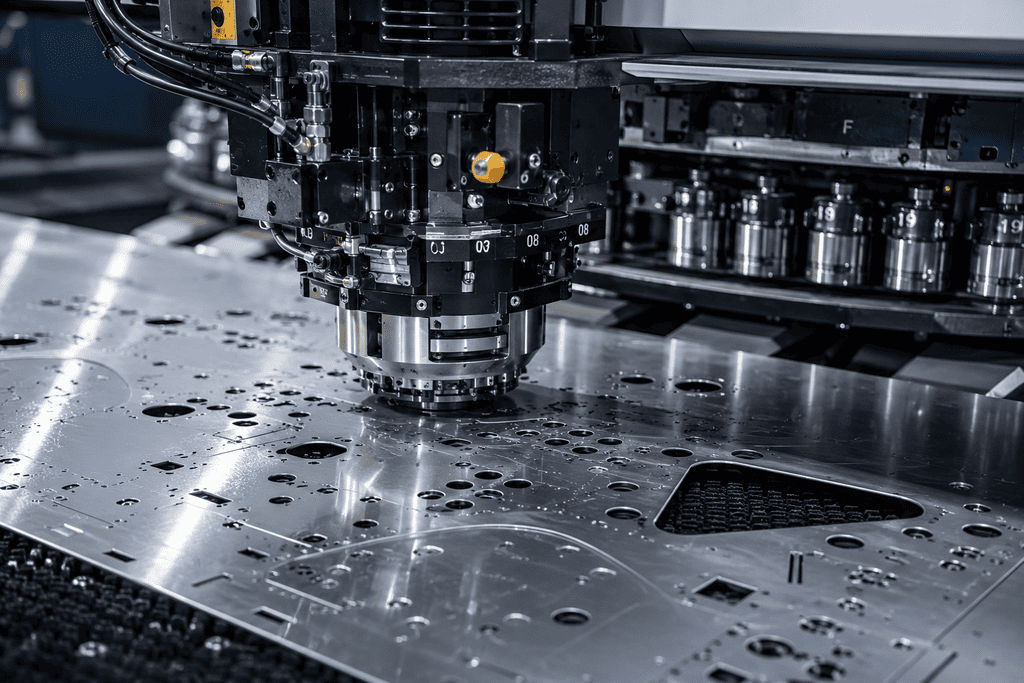
To increase the tool service life, it is necessary to follow some basic rules:
- Knowledge and safety: The operator must be familiar with the machine, possess basic knowledge of stamping theory, and be informed about previous and current operations performed on this equipment. During operation, all safety rules and regulations must be properly observed;
- Clearance: Select the correct clearance depending on the material thickness and its physical properties;
- Tool maintenance: Timely regrinding of the tool followed by its demagnetization;
- Lubrication: Regularly lubricate the tool or use coated tools;
- Alignment check: Periodically check adapters, punch holders, and the alignment between the punch and die;
- Programming: Select the correct punching modes when programming.
Important Information for Programming
When programming external cutouts and corners, keep in mind that their processing zone should extend beyond the edges of the part by 2…3 mm.
If a slot or hole cannot be processed in a single hit, its processing should be programmed in such a way that the tool always operates with the larger part of its surface during consecutive hits. This also applies to contouring.
Some tool manufacturers recommend programming the processing so that the tool utilization rate is at least 70%. If under any circumstances it is impossible to program processing with these conditions, you must use a tool with a smaller area, either separately or in combination with another tool.
Dependence of the Minimum Punch Size on Material Thickness
Material thickness is a critical aspect, especially when the diameter or one of the sides of the holes is close to the thickness of the sheet metal being processed.
- Basic rule: The punch diameter should not be less than the sheet thickness.
- Exceptions: This is possible on hydraulic punching presses, as the punching speed is adjustable.
- Soft materials: In certain cases, it is possible to punch material with a thickness greater than the hole diameter—for example, when punching soft materials such as aluminum or copper. However, note that in this case, the tool service life will be somewhat shorter.
Determining Optimal Clearance
The clearance between the punch and die significantly affects tool service life, as well as the accuracy and smoothness of the processed part. Clearance is determined based on the physical properties and thickness of the material. Proper clearance adjustment ensures high-quality parts while maintaining optimal tool wear.
- Insufficient clearance produces holes of ideal quality, but high load on the tool results in maximum wear.
- Increased clearance causes burrs on the parts, and the edges of the holes turn out uneven.
Table for Determining Optimal Clearance
Optimal clearance is determined depending on the material and its thickness:
| Material | Material Thickness | Minimum | Standard | Maximum |
|---|---|---|---|---|
| Aluminum / Copper / Brass (Tensile strength: 20÷25 kg/mm²) | Up to 2 mm | 8% | 10% | 12% |
| From 2 mm to 4 mm | 10% | 12% | 15% | |
| Over 4 mm | 12% | 15% | 20% | |
| Mild steel (Tensile strength: 30÷40 kg/mm²) | Up to 2.5 mm | 15% | 18% | 20% |
| From 2.5 mm to 5 mm | 18% | 22% | 25% | |
| Over 5 mm | 20% | 25% | 30% | |
| Stainless steel (Tensile strength: 60÷80 kg/mm²) | Up to 1.5 mm | 15% | 20% | 22% |
| From 1.5 mm to 3 mm | 18% | 22% | 25% | |
| Over 3 mm | 20% | 25% | 28% |
*Note: Clearance values are specified as a percentage of the processed material thickness.
Punch Coating
To improve operational performance, the punch surface can be coated with a special protective coating. This increases wear resistance and lubricity of the tool. Depending on the tasks at hand, each tool manufacturer offers several types of coatings.
Tool Sharpening
Professional sharpening guarantees long and consistent performance of punching tools. Tool sharpening is an easy, fast, and economical process that can be performed by operators using grinding machines and accessories. Thanks to a wide range of machines, tooling, and instructions, all customer needs can be met.
Sharpening Recommendations:
- Timeliness: It is recommended to sharpen at the first sign of wear (appearance of a cutting edge radius exceeding 0.15 mm) to minimize material loss.
- Grinding method: Tool manufacturers usually recommend using CBN grinding, known as "cool cutting", or soft grinding.
- Wheel parameters: A standard corundum wheel with hardness from D to J and grain size from 45 to 60 can be used for grinding.
- Cooling: Removal of small amounts of material must be performed with intensive cooling. Non-compliance with this rule can lead to loss of strength, microcracks, and tool breakage.
- Demagnetization: After grinding, tools must be demagnetized to avoid slug pulling/ejection issues.
- Length compensation: Set up punches taking into account length reduction compensation resulting from regrinding.
- Thick materials: For heavy material thickness, use punches with increased shear angle and dies with larger clearance.
Sharpening Punches with Shear Angles
Advantages:
- Noise reduction
- Punching force reduction
- Improved slug removal
- Reduced shock load
There are several types of shear angles designed for specific punching conditions:
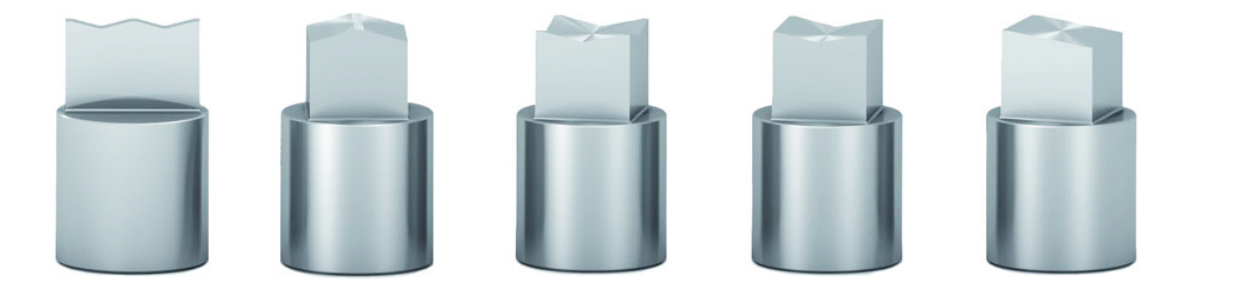
| for tool sharpening and large thicknesses |
for balanced load and large thicknesses |
for small thicknesses – large shape nibbling |
for small thicknesses – small shape nibbling |
for small thicknesses – small shape nibbling |
Troubleshooting
Troubles may arise during tool operation. Below is a table for quick diagnostics and troubleshooting:
| Problem | Possible Cause | Solution |
|---|---|---|
| Excessive burrs | • Incorrect clearance between punch and die • Tool wear • Tool components misalignment |
• Replace die • Sharpen or replace tools • Check alignment of tool components |
| Punch or die breakage | • Incorrect clearance between punch and die • Tool wear • Unsuitable punch for the given thickness or incorrect technology |
• Replace die • Sharpen or replace tools • Replace tool or modify technology |
| Punch stripping failure or jamming | • Incorrect clearance between punch and die • Lack of lubrication • Material too hard |
• Replace die • Lubricate tool or use coated punches • Replace springs |
| High tool wear | • Incorrect clearance between punch and die • Hard or abrasive material • Tool components misalignment • Incorrect technology • Incorrect or untimely tool sharpening |
• Replace die • Use coated punches • Check tool alignment • Modify technology • Perform checks and maintenance more frequently • Sharpen timely |
| Slug pulling / ejection | • Insufficient punch length • Punching sheet that is too thin • Slugs sticking due to excess oil • Tool not demagnetized after sharpening |
• Adjust punch length • Use shear punch or special die • Reduce oil supply, wipe off excess, or use lighter lubricant • Always demagnetize tools after sharpening |
| Cutting edge chipping | • Incorrect clearance between punch and die • Tool components misalignment • Slug pulling resulting in double sheet thickness punching • Incorrect technology • Untimely sharpening |
• Replace die • Check tool alignment • Use methods to prevent slug pulling • Modify technology • Sharpen tool timely |


